Black Color Converter About
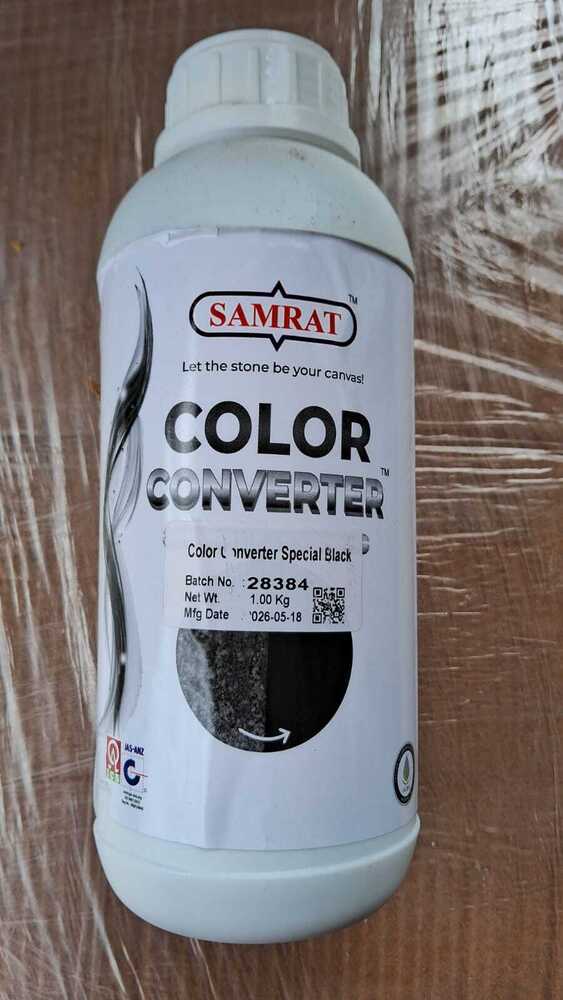
Procure the ace in color technology with our Black Color Converter. Capitalise on its unmatchable, high stability formula-purpose-built for industrial use, especially in textiles. This uncommon liquid converter offers a special black shade with 99% purity and exceptional temperature stability (up to 72C). Readily mixable, it guarantees seamless integration and superior color conversion. Suitable for retailers, suppliers, traders, and wholesalers across India, this industrial-grade solution guarantees consistent results and density (1000 g/cm3). Store in a cool, dry place. Sale packaging: 1-litre plastic bottle. Shelf life: 12 months.
Versatile Application & Machine Features
The Black Color Converter excels in color conversion on a wide variety of applications, lending itself perfectly to textile and industrial uses. As a liquid form solution, it adapts seamlessly to various machinery settings and is engineered for high stability, special black shade, and consistent performance even under temperatures up to 72C. With its readily mixable nature and 99% purity, users can count on uniformity and standout results in any industrial process demanding premium black color.
Sample Policy & Export Details
Our Black Color Converter is available for sampling upon request with clear purchase order procedures. Once the order is finalized, the product is promptly handed over to the client for inspection. We focus on key export markets including India and neighboring regions. Payment terms are flexible and managed efficiently to meet diverse client needs. Reliable handling and streamlined logistics make our converter a preferred choice for large-scale industrial buyers and traders.
FAQ's of Black Color Converter:
Q: How is the Black Color Converter used in textile applications?
A: The Black Color Converter is added to the textile color conversion process to achieve a special, deep black shade with high stability. Its liquid form allows it to mix easily with other industrial solutions, ensuring even coloring and excellent results.
Q: What distinguishes this color converter from others in the market?
A: It delivers an unmatchable black shade, offers high temperature stability (up to 72C), and boasts 99% purity, making it a superior solution for demanding industrial processes. The converter's ready-to-mix feature ensures easy and efficient application.
Q: Where should the product be stored for optimal performance?
A: To maintain shelf life and product stability, the Black Color Converter should be stored in a cool and dry place, away from direct sunlight and heat sources.
Q: When can customers expect delivery after the purchase order is placed?
A: Once a purchase order is confirmed, the product is prepared and handed over promptly for delivery, ensuring reliable and timely supply to customers.
Q: What is the recommended process for using this converter in industrial machinery?
A: Simply add the required amount of the liquid color converter into the designated phase of your color or dyeing process, ensuring proper mixing for consistent coloration across your substrates.
Q: What are the key benefits of choosing this Black Color Converter?
A: Users benefit from its uncommon stability, exceptional color performance, ease of mixing, high purity, and suitability for both textile and diverse industrial applications-all supported by efficient packaging and export logistics.




 Send Inquiry


 Send Inquiry
 Send Inquiry
 Send SMS
